Delivery of four ultrafiltration units for food processing company in Northern Norway
Logisticon Water Treatment recently supplied four large-scale ultrafiltration (UF) units to a production facility of an international food company in northern Norway. The project is a continuation of previous successful implementations of Logisticon's UF technology at other locations belonging to this customer.
Process challenge: reliable, particle-free water
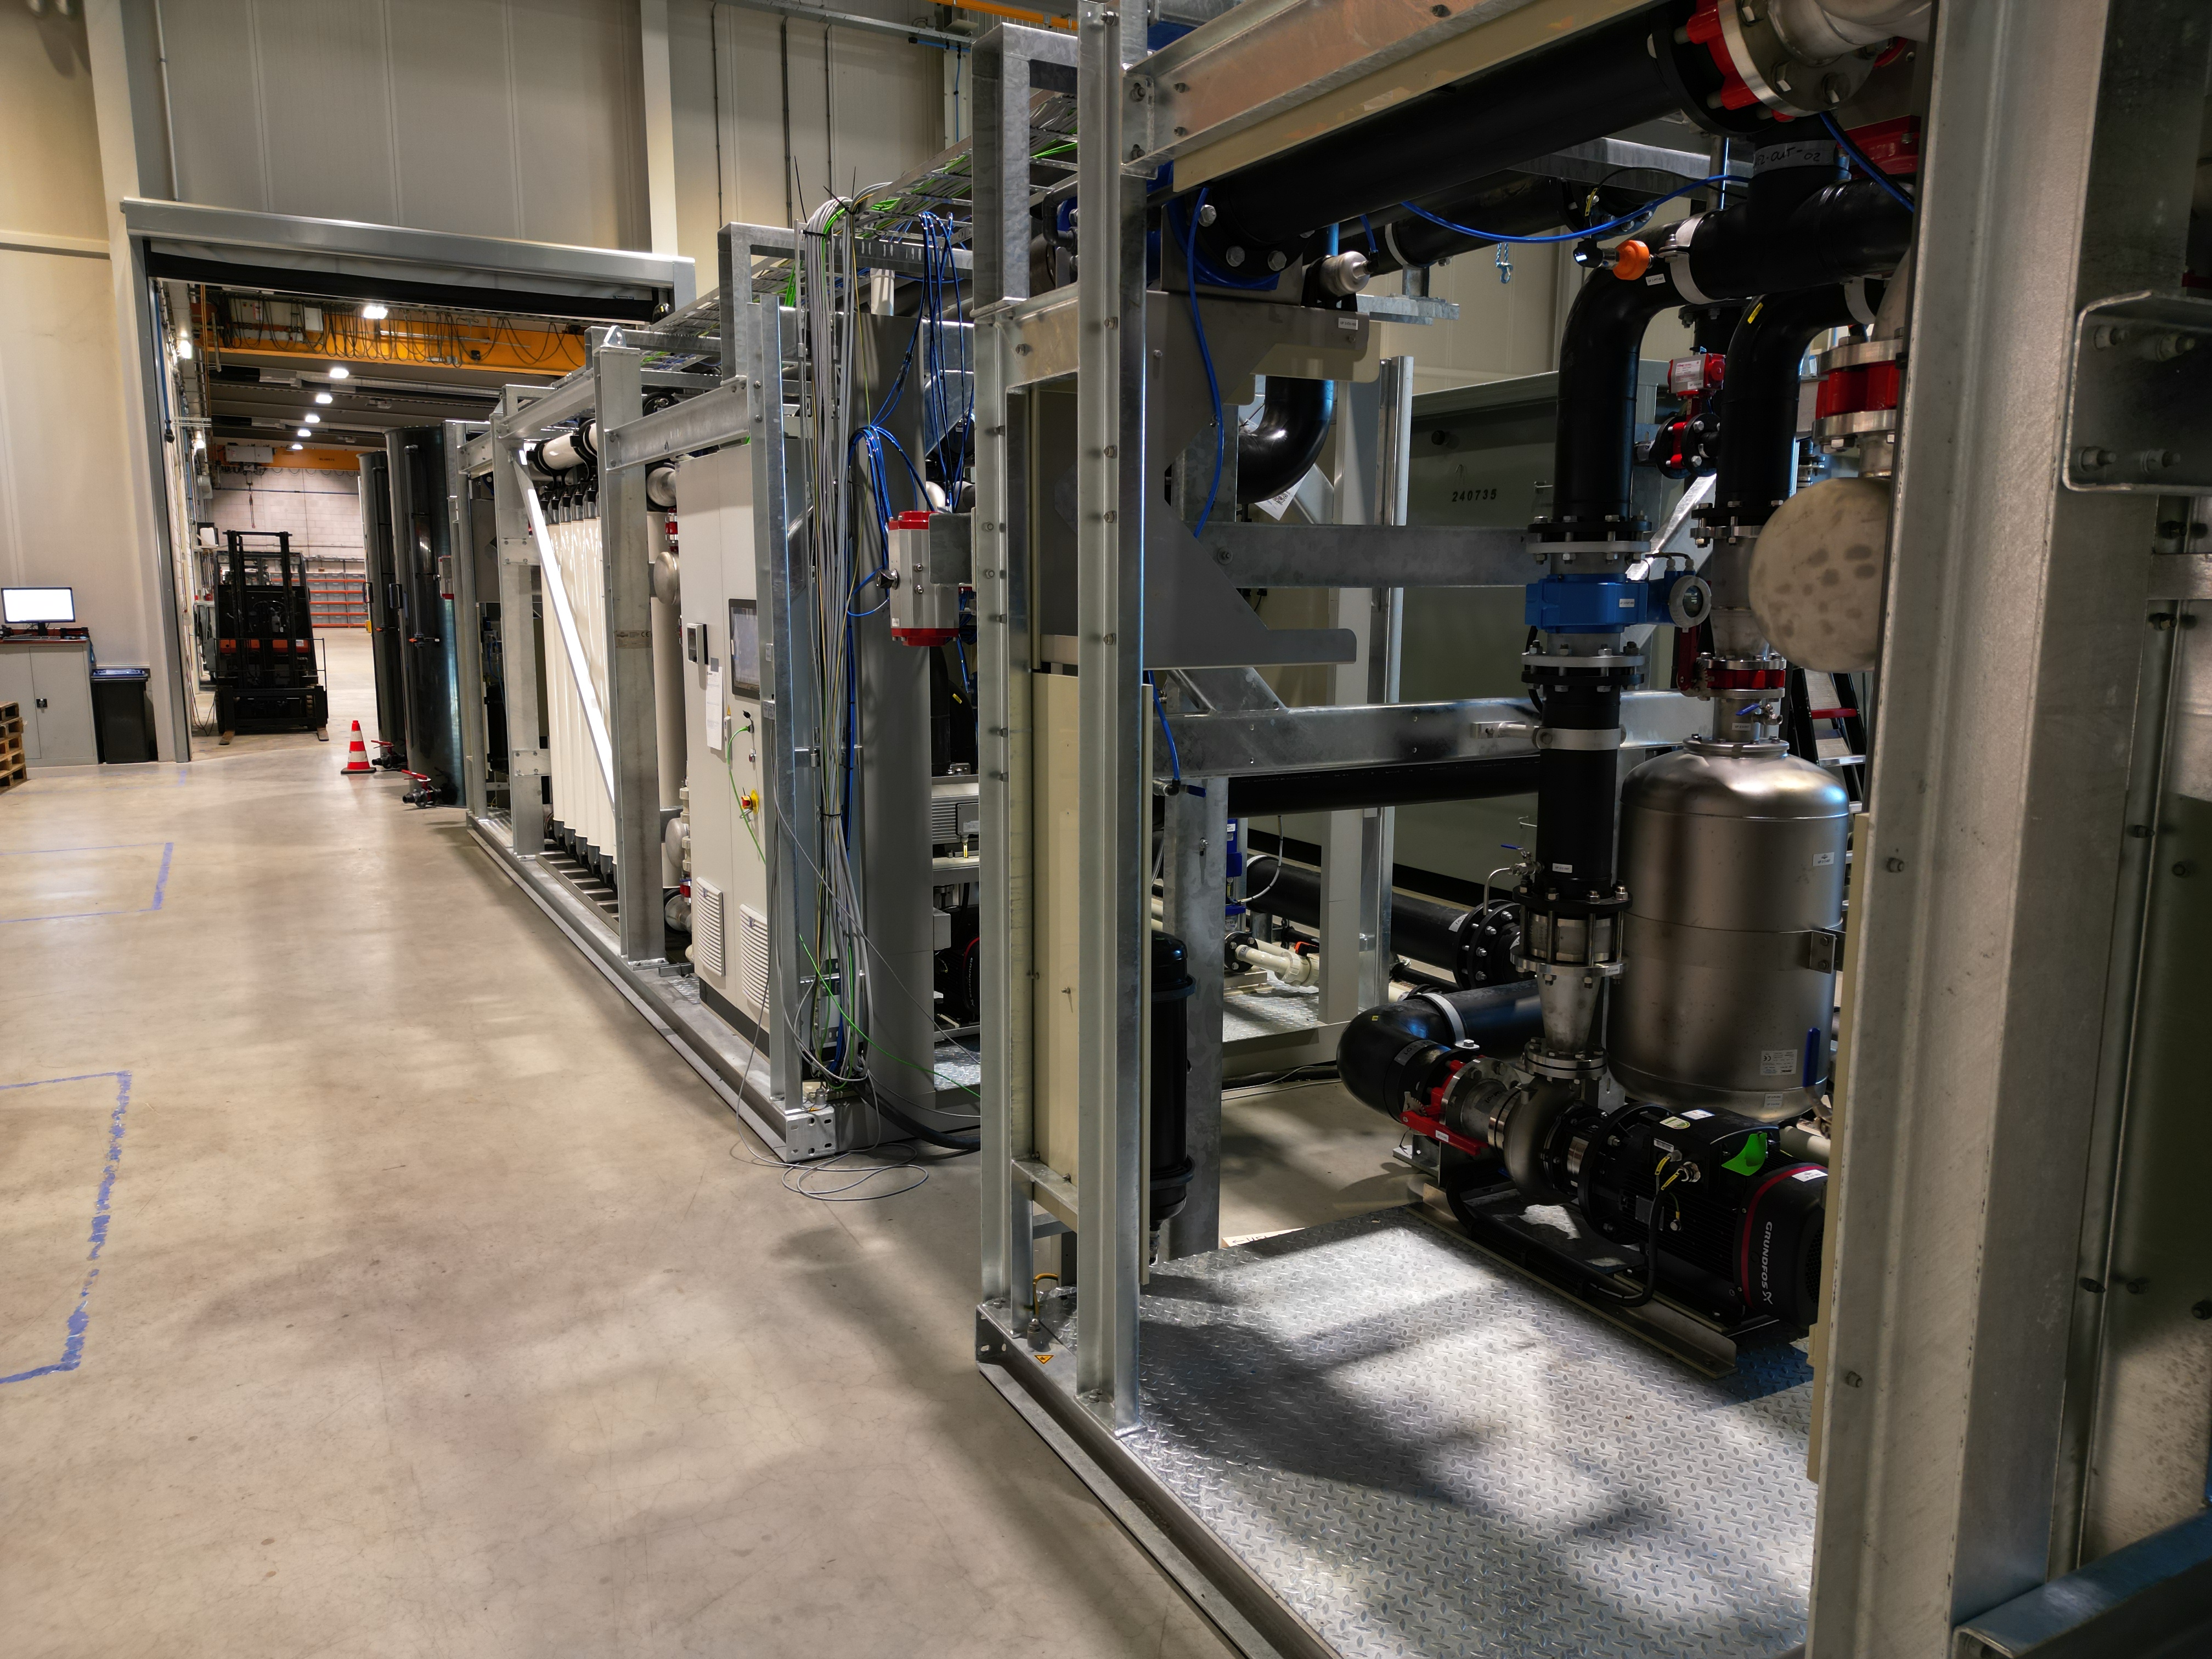
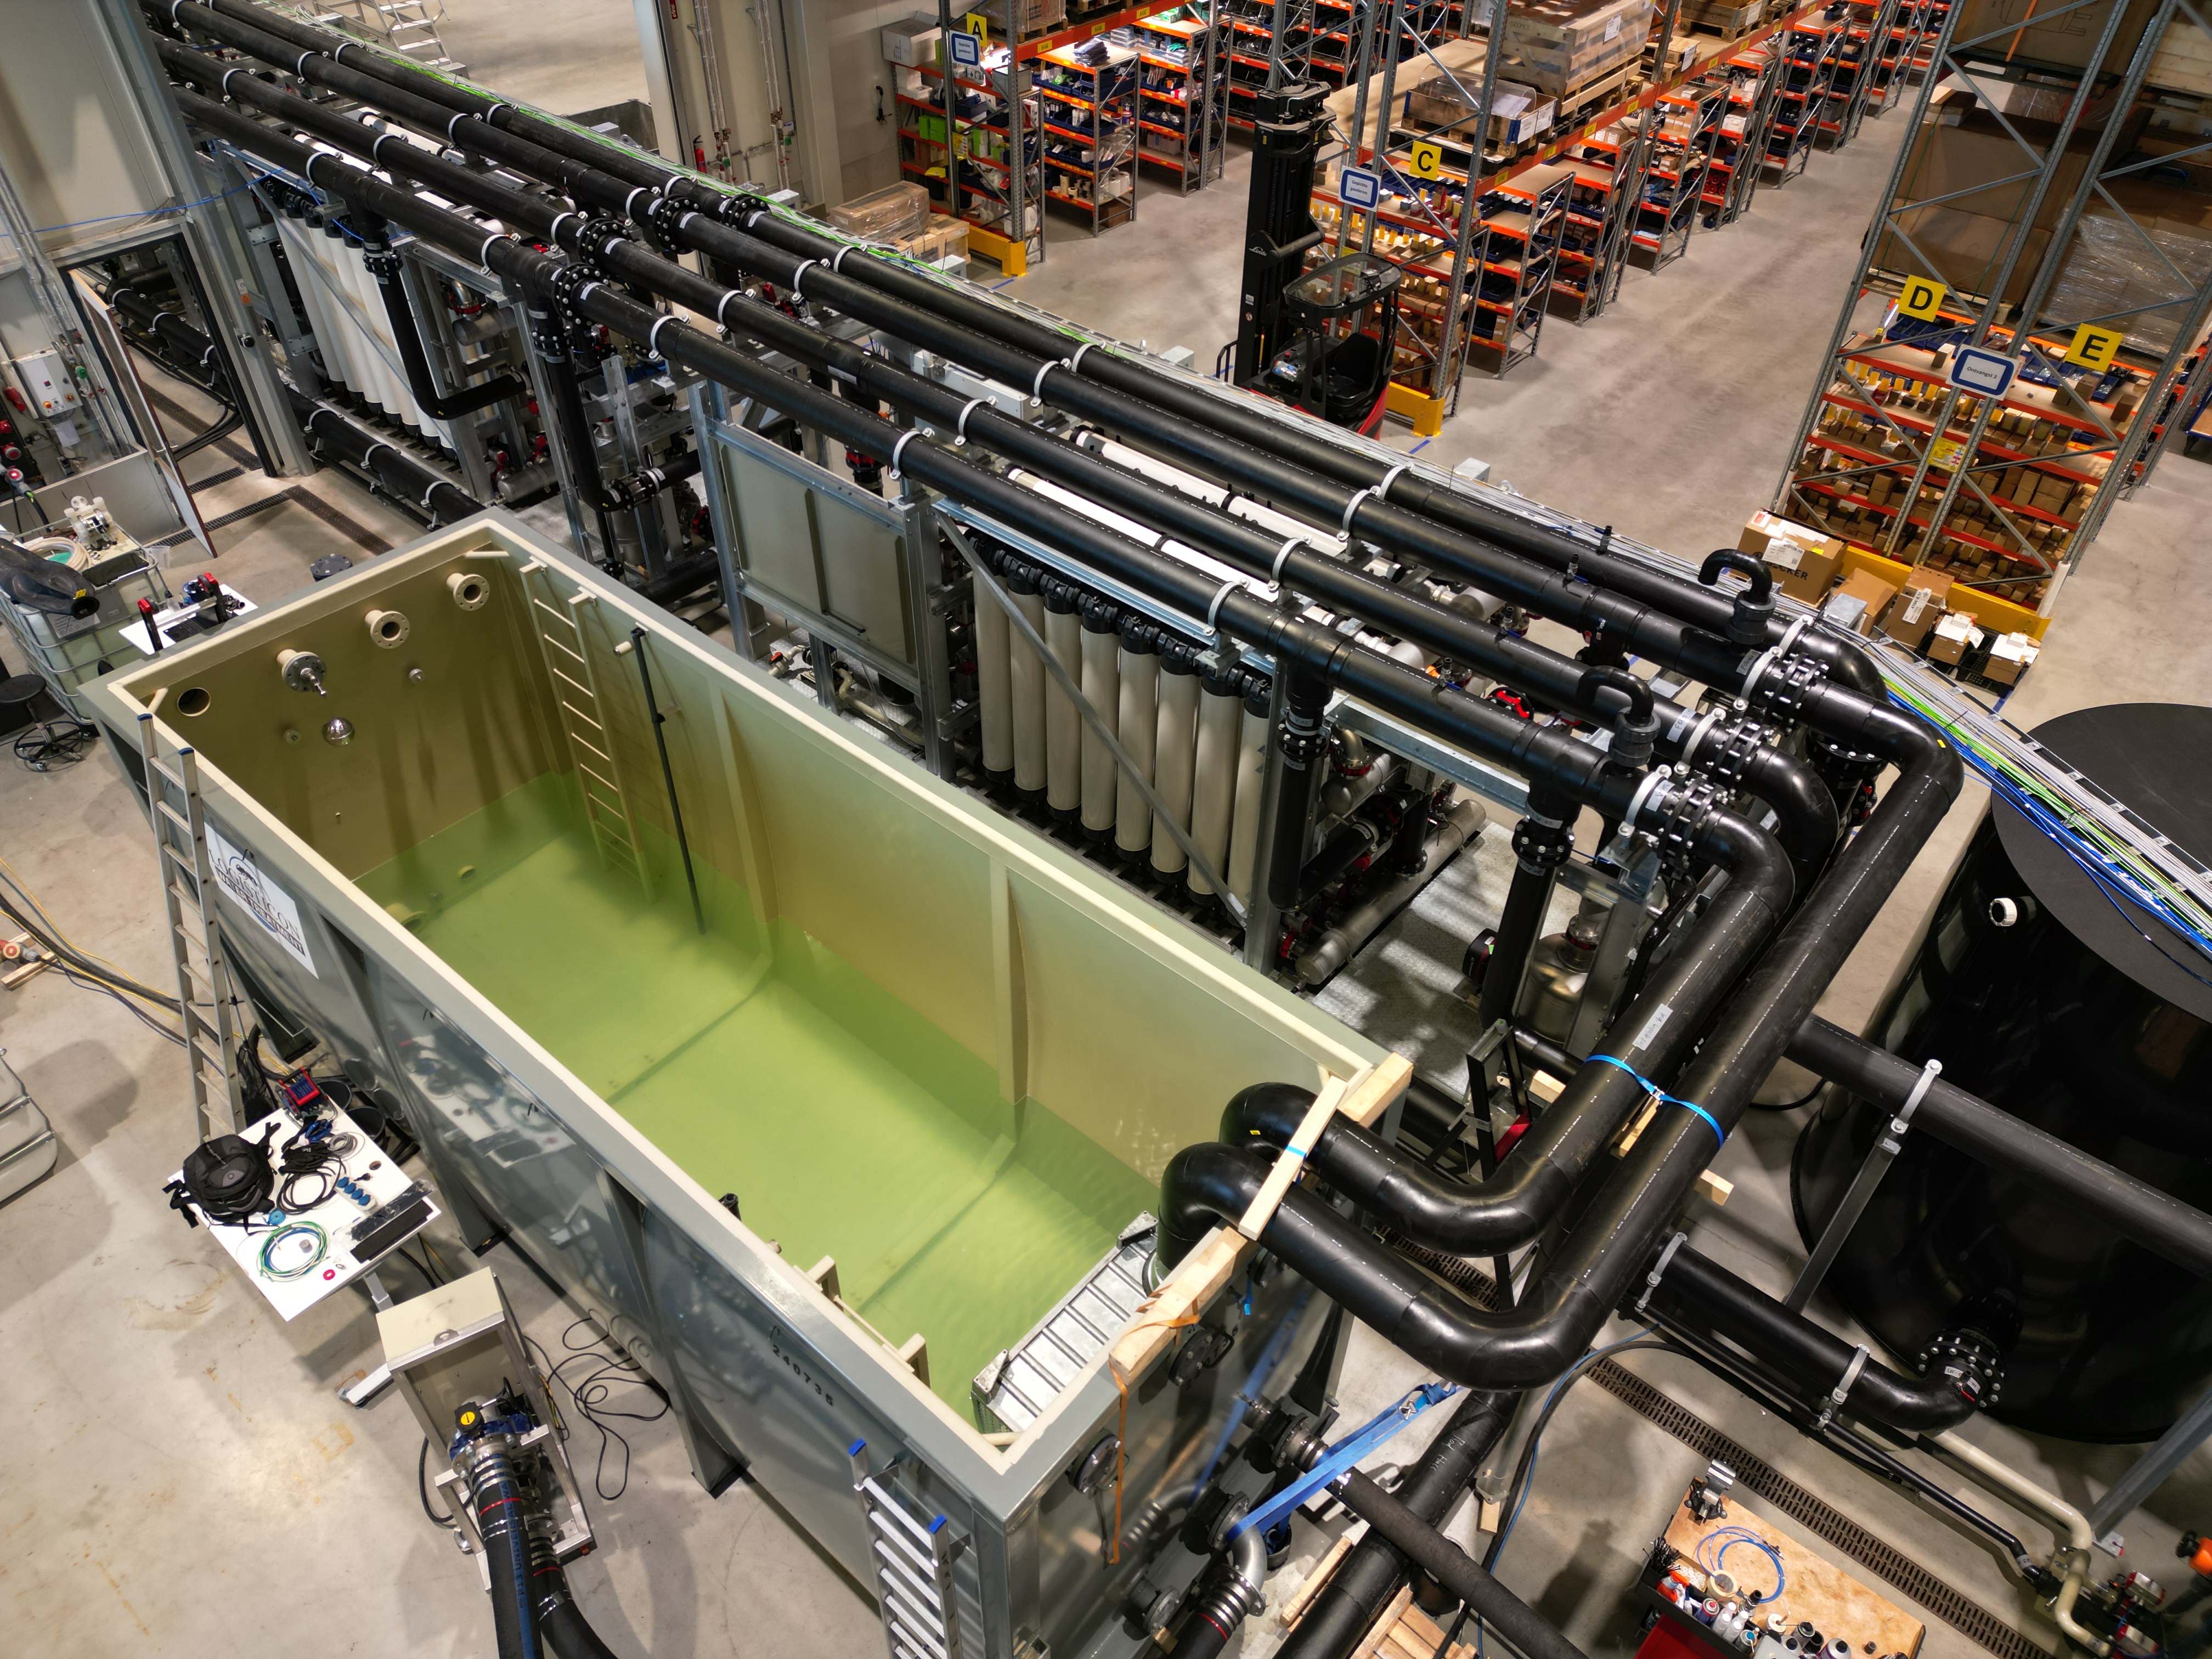
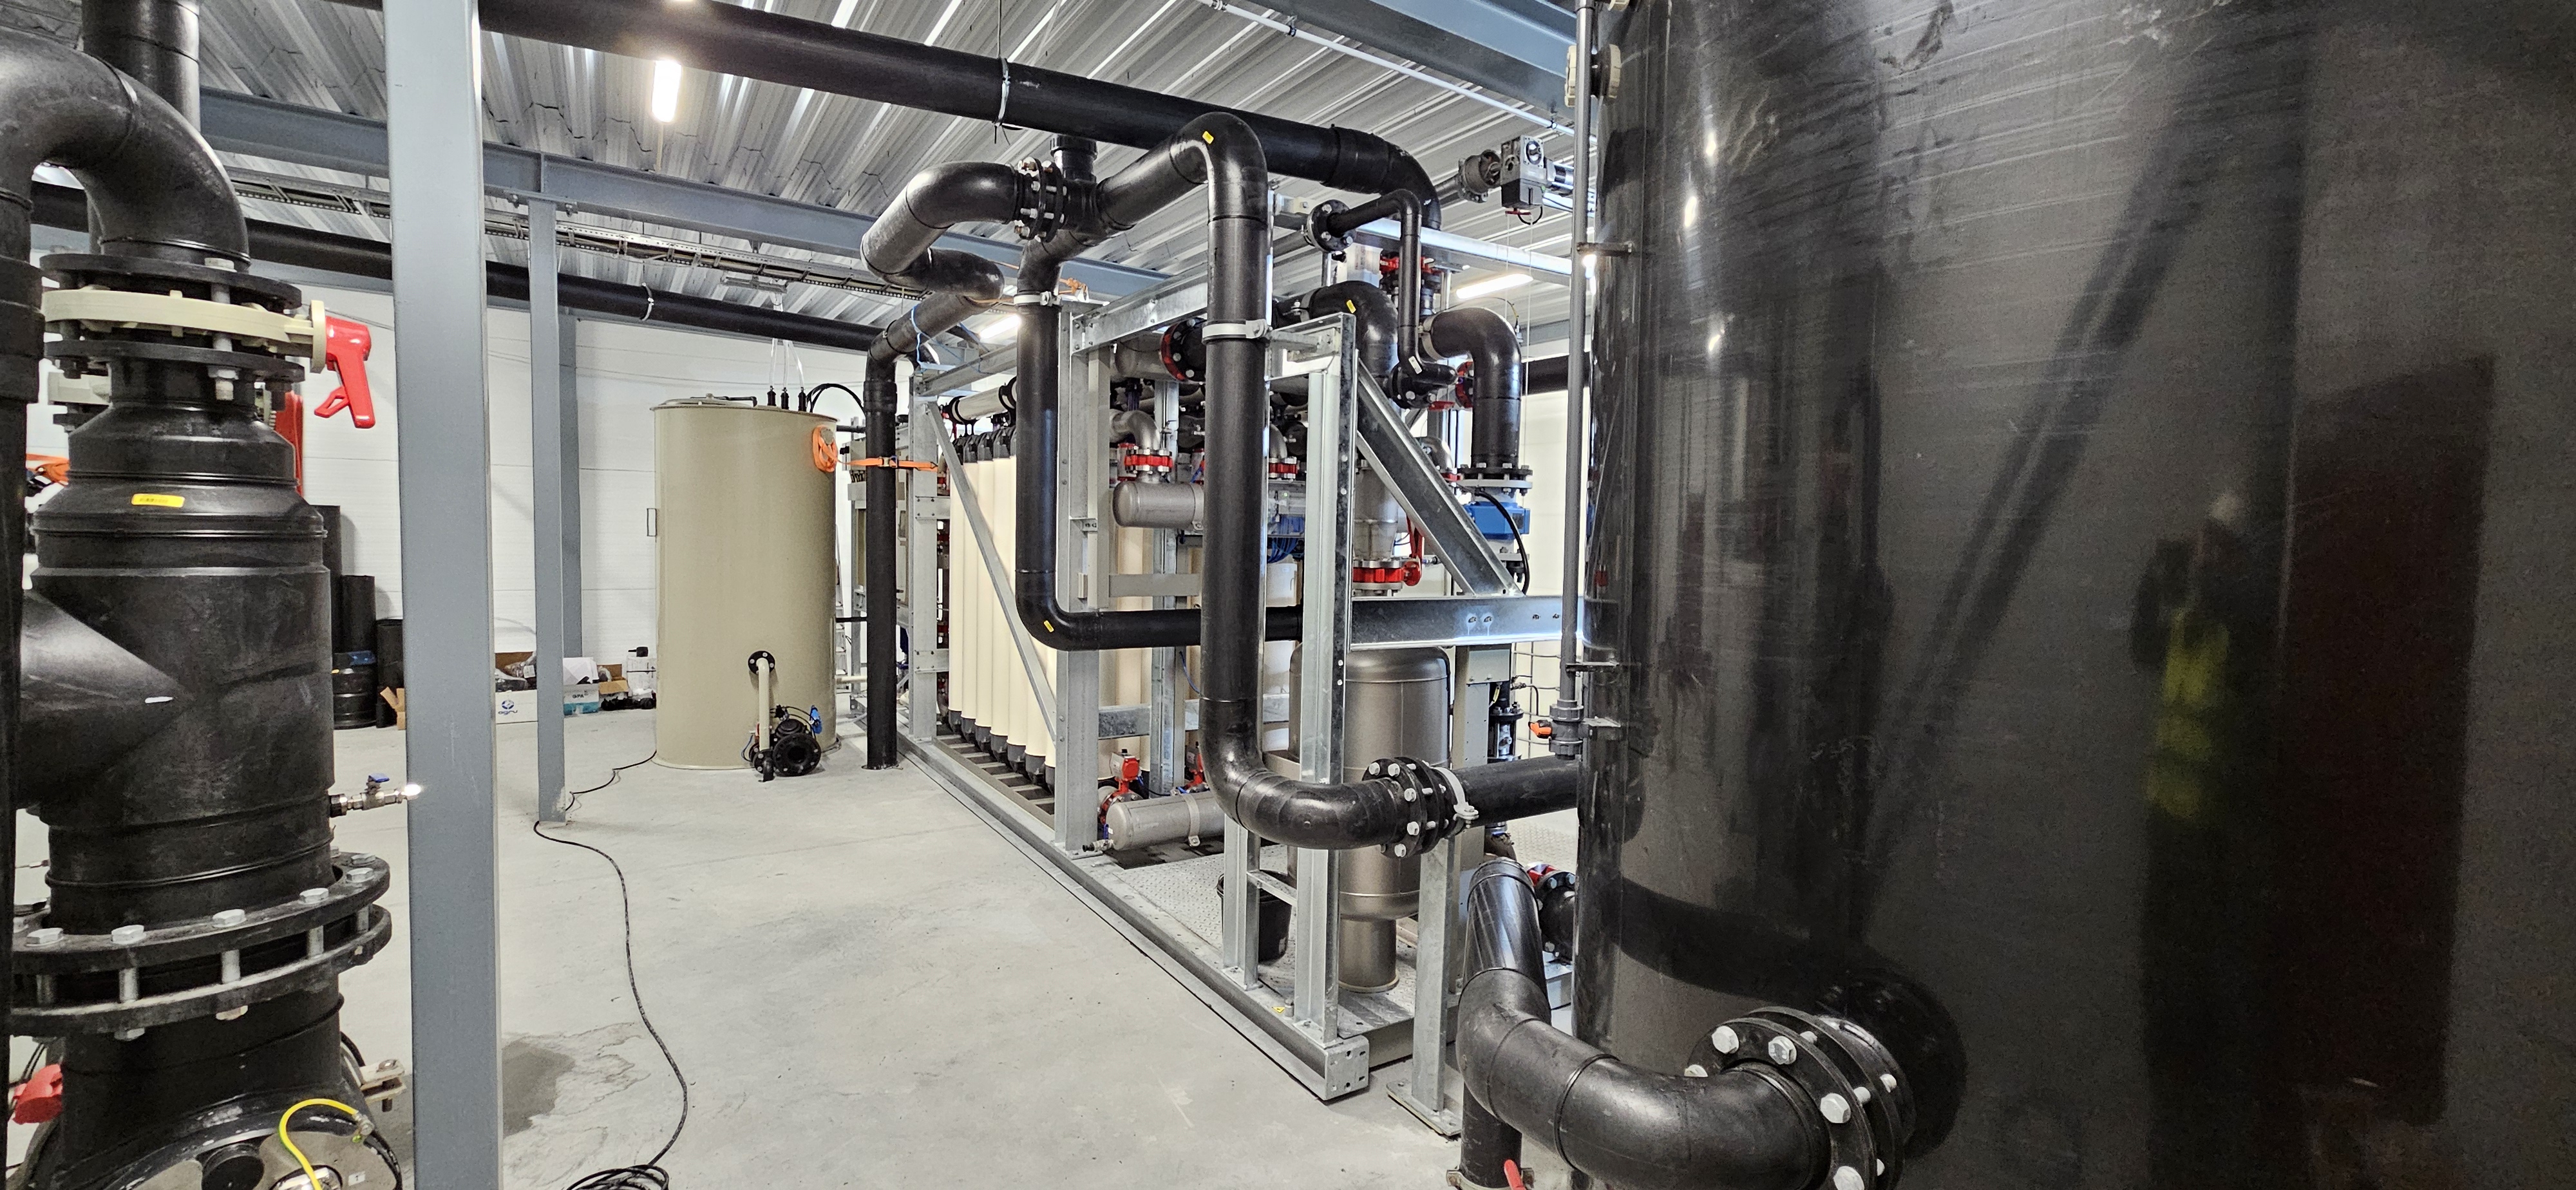
In the food industry, the availability of hygienically reliable process water is crucial. The supplied water had to be free of particles, bacteria, and viruses in order to meet the required quality standards. Ultrafiltration is a suitable solution for this. The technique uses membranes (DuPont™ IntegraTec™) with a pore size of approximately 0.02 μm. The water is forced through these membranes under pressure, trapping solids and microorganisms and allowing only particle-free permeate to pass through.
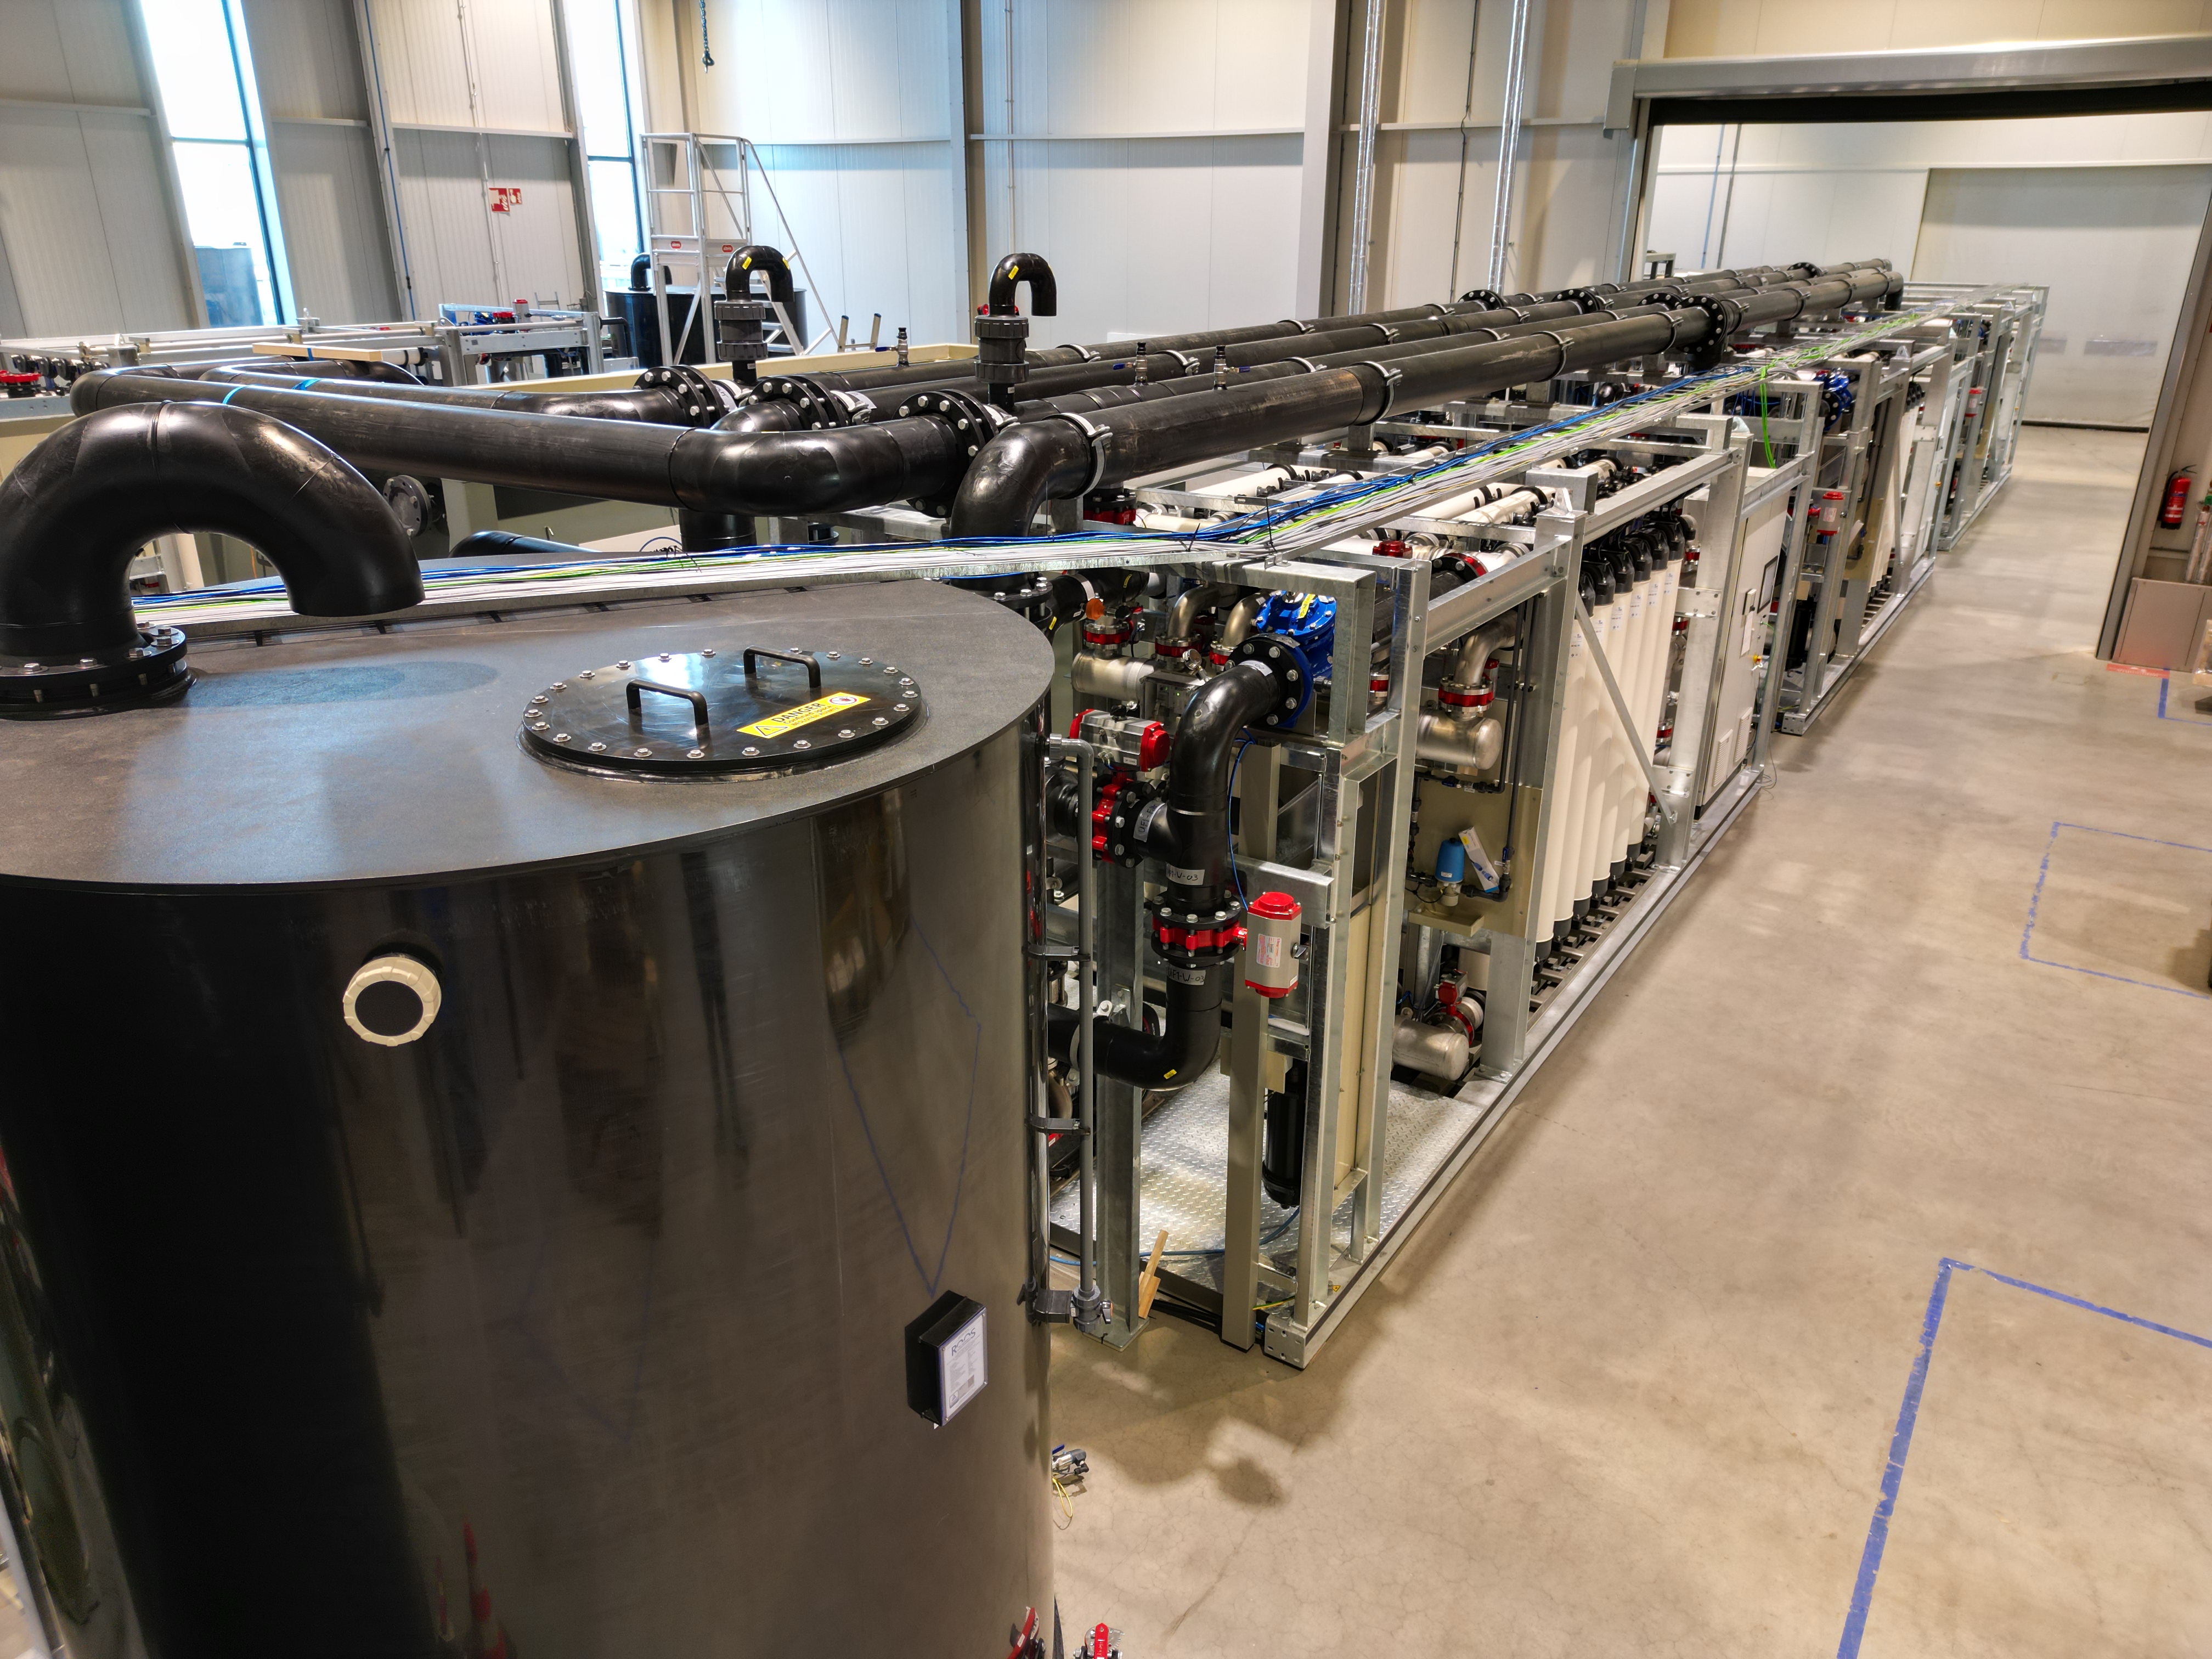
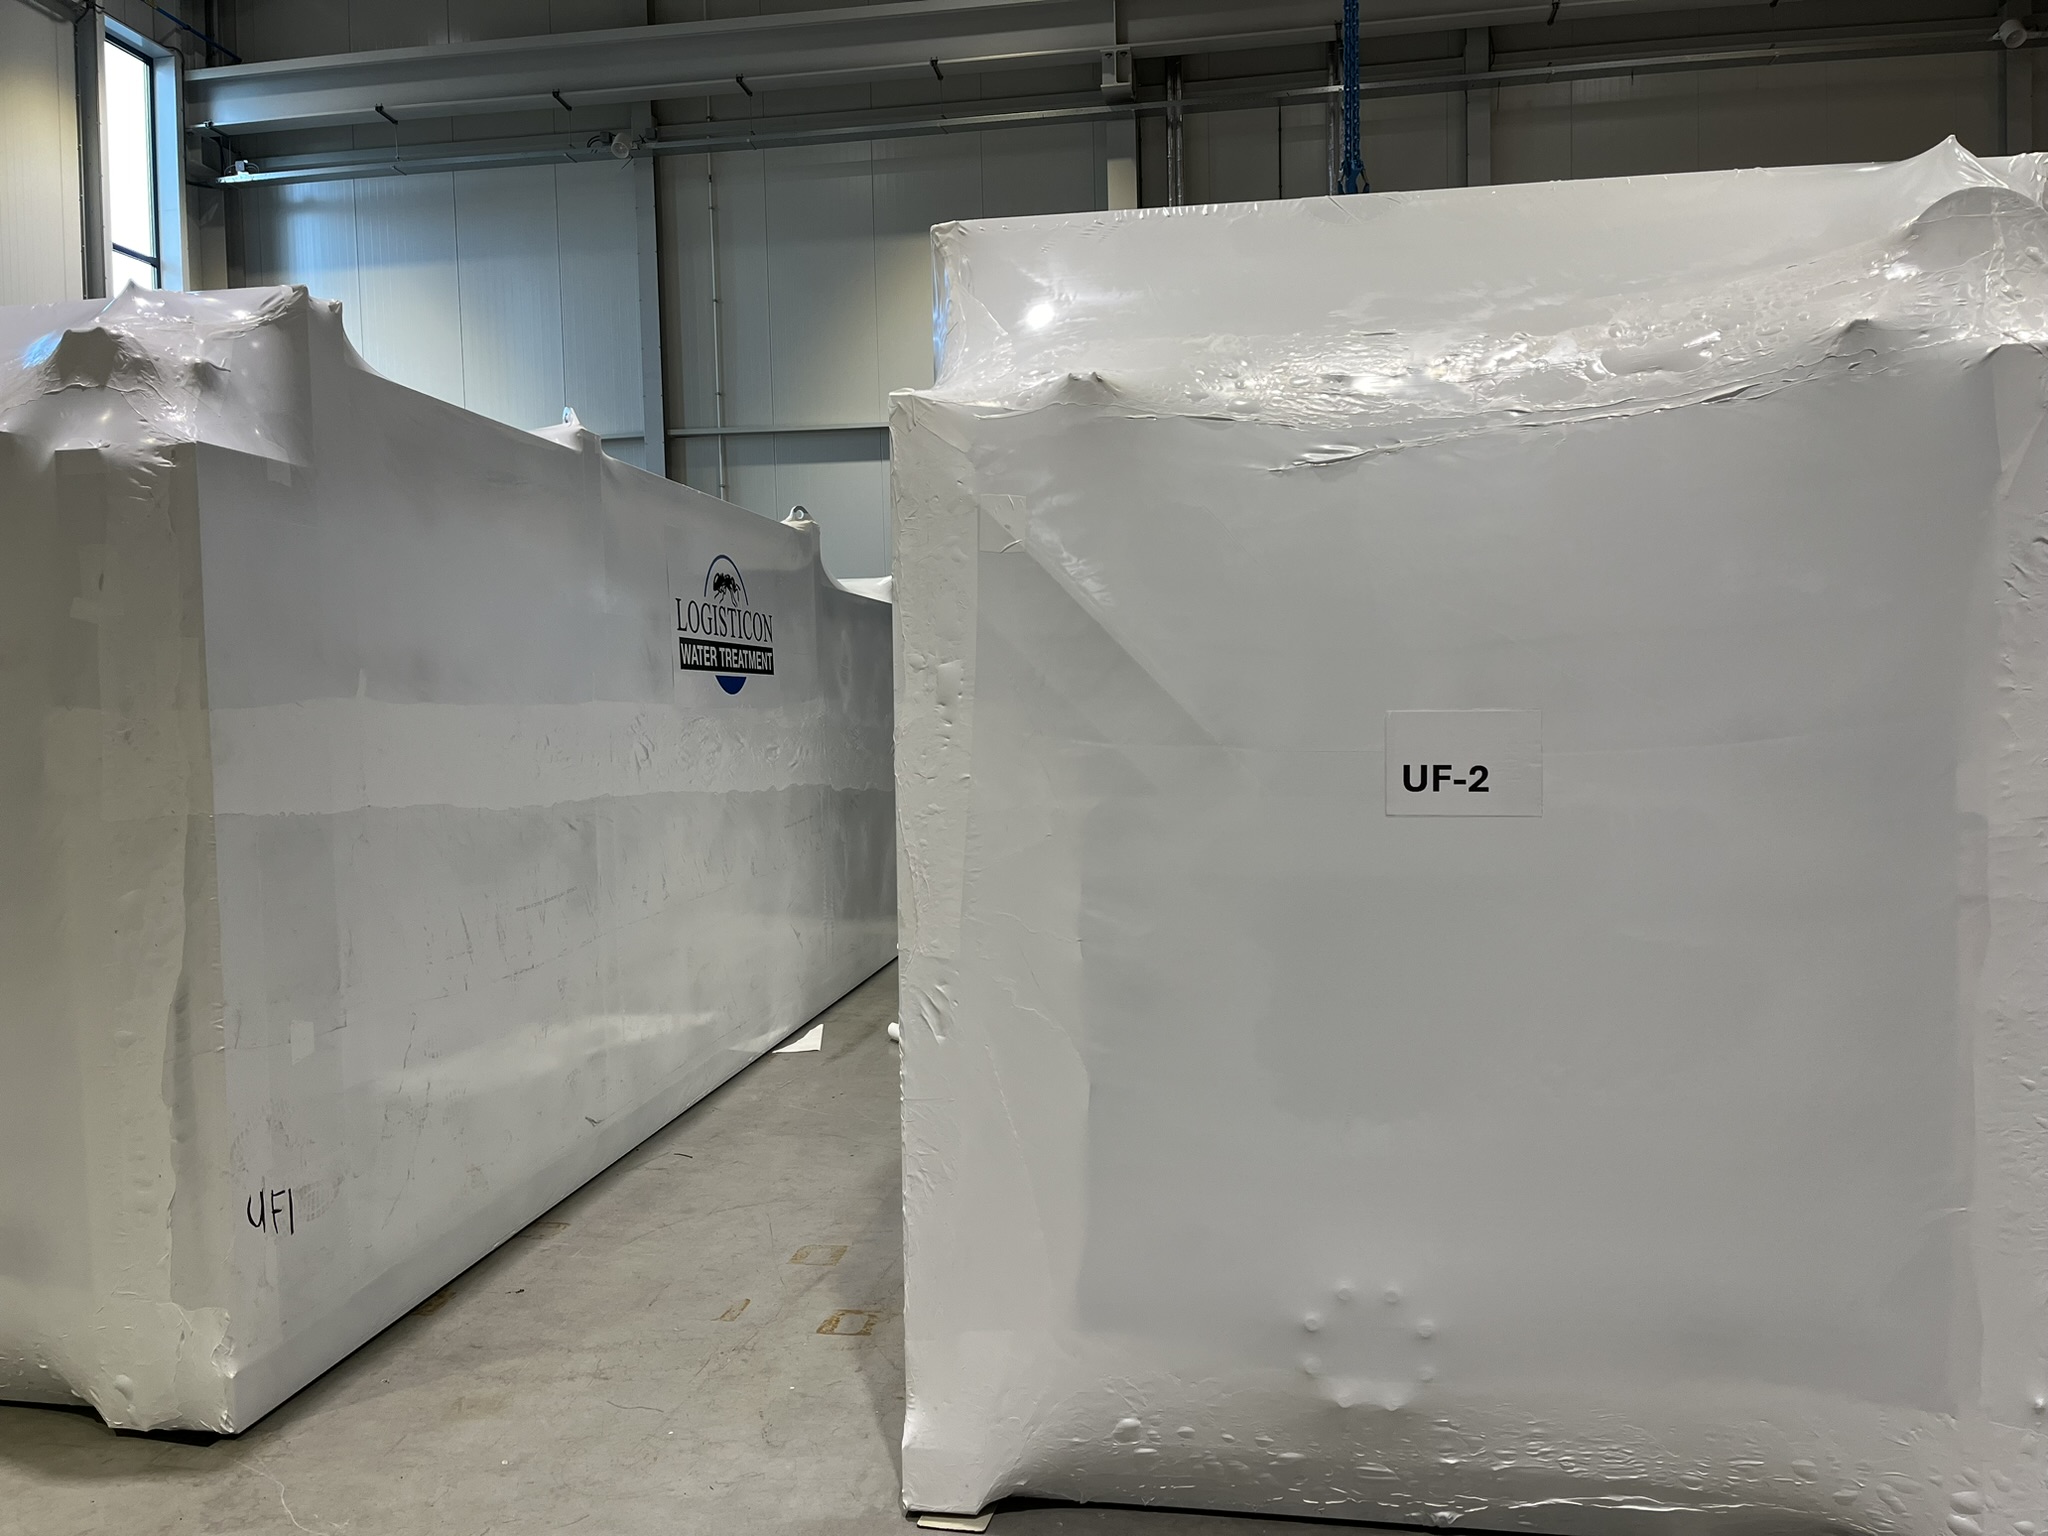
For this project, a system consisting of three linked UF units and one independent stand-alone unit, each with a capacity of 200 m³/h, was requested. However, the challenge was not primarily in the design or technology, but in the complex logistical conditions.
Logistical and climatic conditions
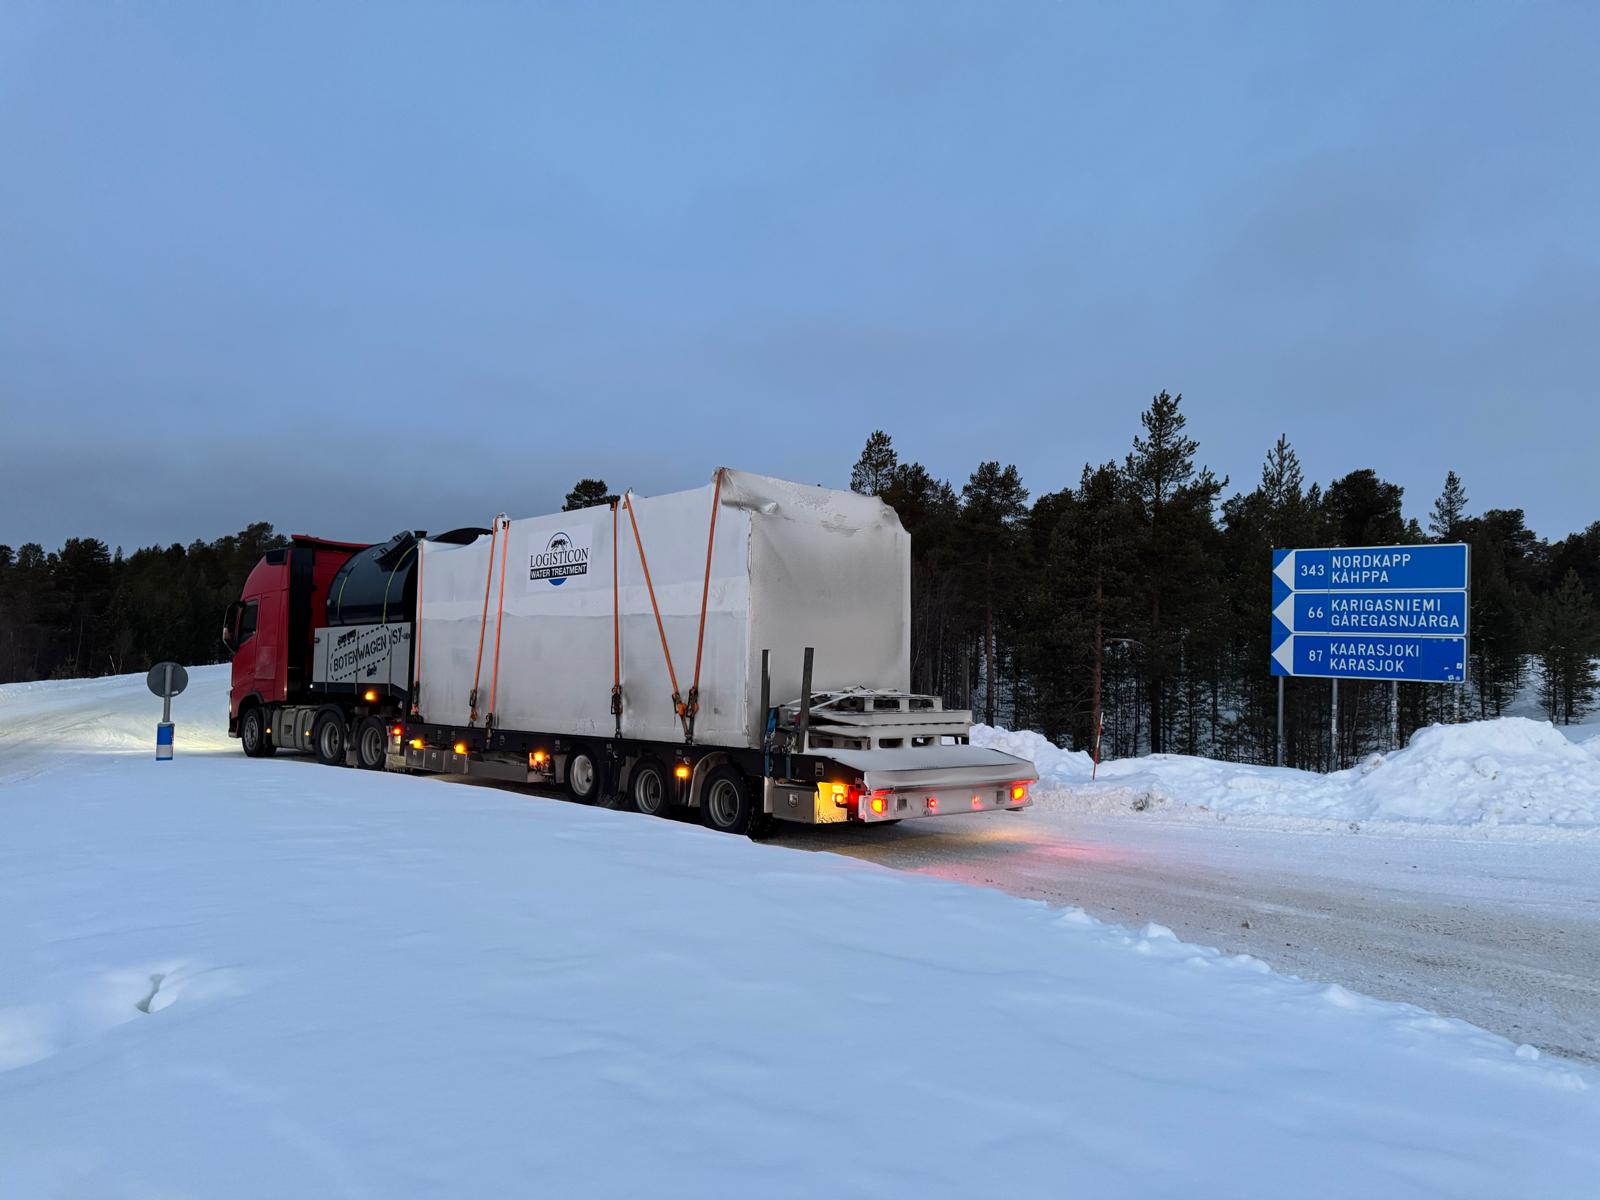
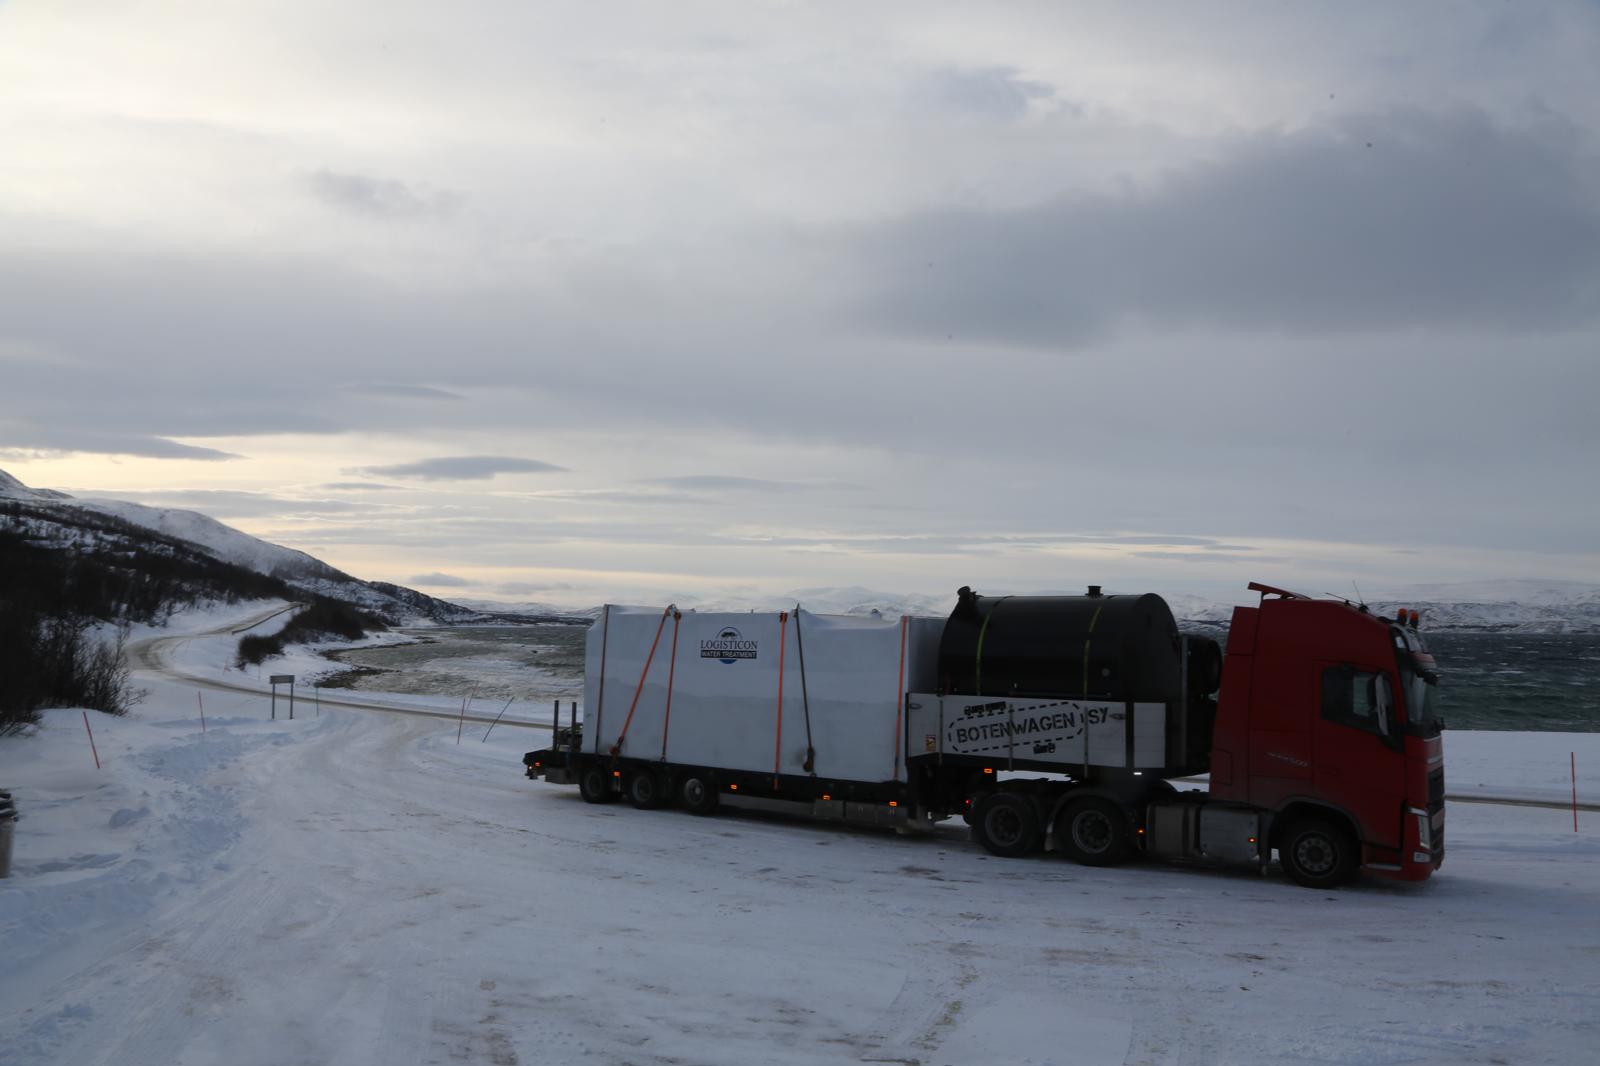
The installation was transported during the winter months, over snow-covered roads in a region where temperatures can drop to -30 to -40°C. Because the equipment cannot withstand prolonged exposure to temperatures below -20°C, the transport process had to be carefully planned and monitored.
The units were fully prefabricated, tested, and equipped with all necessary couplings and piping in the Netherlands. After functional approval (FAT), the systems were carefully dismantled for transport. During transport, continuous monitoring was carried out via GPS trackers, and the weather conditions along the route were analyzed several times a day in order to adjust the route where necessary. The lowest temperature measured during transport was -14°C — well within the predetermined safety margin.
Installation and commissioning on site
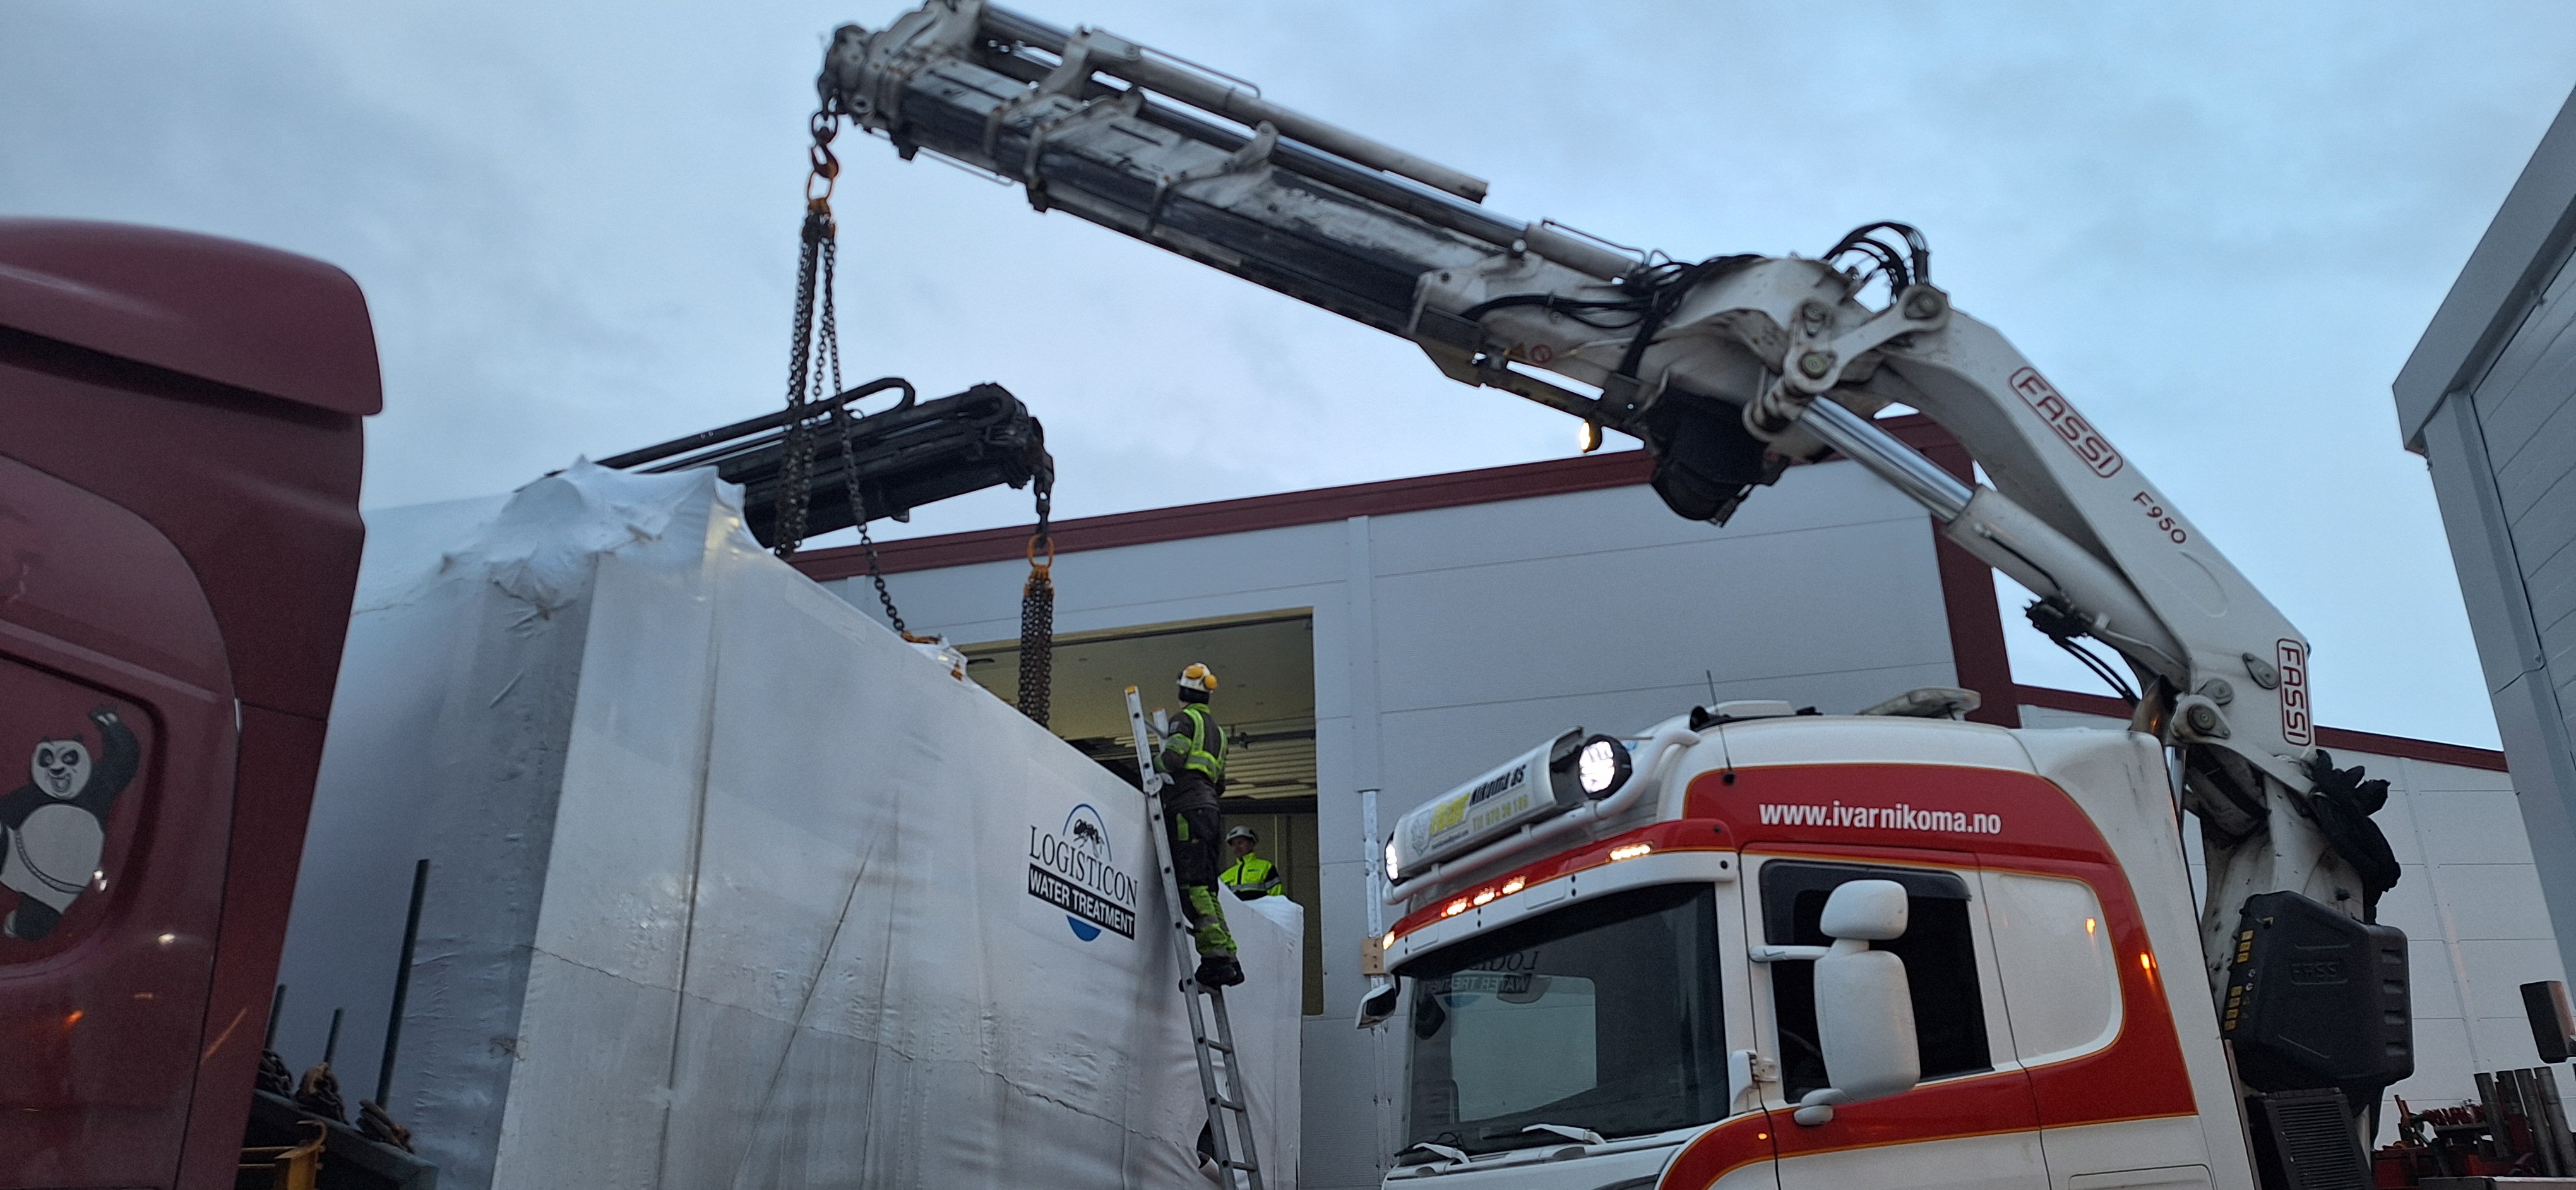
After arrival in Norway, the units were mechanically assembled and connected by the customer. The Logisticon service team then supervised the commissioning of the installation. Thanks to clear preparation and previous experience with this customer, this process ran efficiently and without any significant complications.
Technological advantages
The four ultrafiltration units offer a scalable solution for the production of reliable process water. Thanks to their modular design, the units can be easily integrated into existing process lines. The stand-alone UF unit also offers flexibility for future expansion or alternative use within the installation. This solution therefore contributes to a stable and sustainable production environment within the food industry.